Customer Success Stories

Built for a customer

CrowFootUSA: Made-to-Size Crowfoot Wrenches

The customer asked our team to create a custom crowfoot wrench configuration and set up the sales pipeline behind it: the website, wrench designs, safety factors, materials, machining vendors, packaging, product testing and validation, and drop shipping.

The result is CrowFootUSA, which makes crowfoot wrenches to your size, from 1/4" to 2" drive. Every wrench is sized for the torque its drive is built for: the jaw wall, neck and plate thickness keep the steel below its yield point at 1-1/2 times that torque, so big wrenches come out heavy-duty.

They're cut from 4130 or 4140 chromoly, heat treated to 42–48 HRC, finished to size and laser etched with the torque correction factor for your wrench length.

What our team delivered

  • Website and configurator
  • Wrench designs
  • Safety factors
  • Material selection
  • Wrench sourcing
  • Machining vendors
  • Shop fabrication
  • Post-processing
  • Torque capacity validation
  • Product testing
  • Packaging
  • Supply chain
  • Drop shipping
Visit crowfootusa.com

What it offers

  1. 1.Custom crowfoot wrenches for any job, 1/4" to 2" drive, any opening
  2. 2.Multi-head crowfoots: up to four sizes on one drive
  3. 3.Online configurator to build the right crowfoot for the job
  4. 4.Tether hole for a lanyard, so the wrench stays with you
  5. 5.Etched QR code for the torque correction table and your choice of traceability data
  6. 6.12-point flare-nut jaws for extremely tight spaces
  7. 7.Robust, low-clearance thin profile
  8. 8.Custom reach lengths

Example configuration

1-1/2" open-end crowfoot, 3/4" drive

Part
CF-34-OE-1.5000
Opening
1-1/2" open end (1.500 across flats)
Drive
3/4" square
Drive center to opening center
2.320"
Jaw wall
.858"
Plate thickness
.500"
Overall size
5.041" × 3.216"
Material
AISI 4140 steel, heat treated to 42–48 HRC
Finishing
Opening and drive finished to size after heat treat; black oxide
Etching
Size, E dimension, and torque correction factor (0.838 at a 12" wrench)
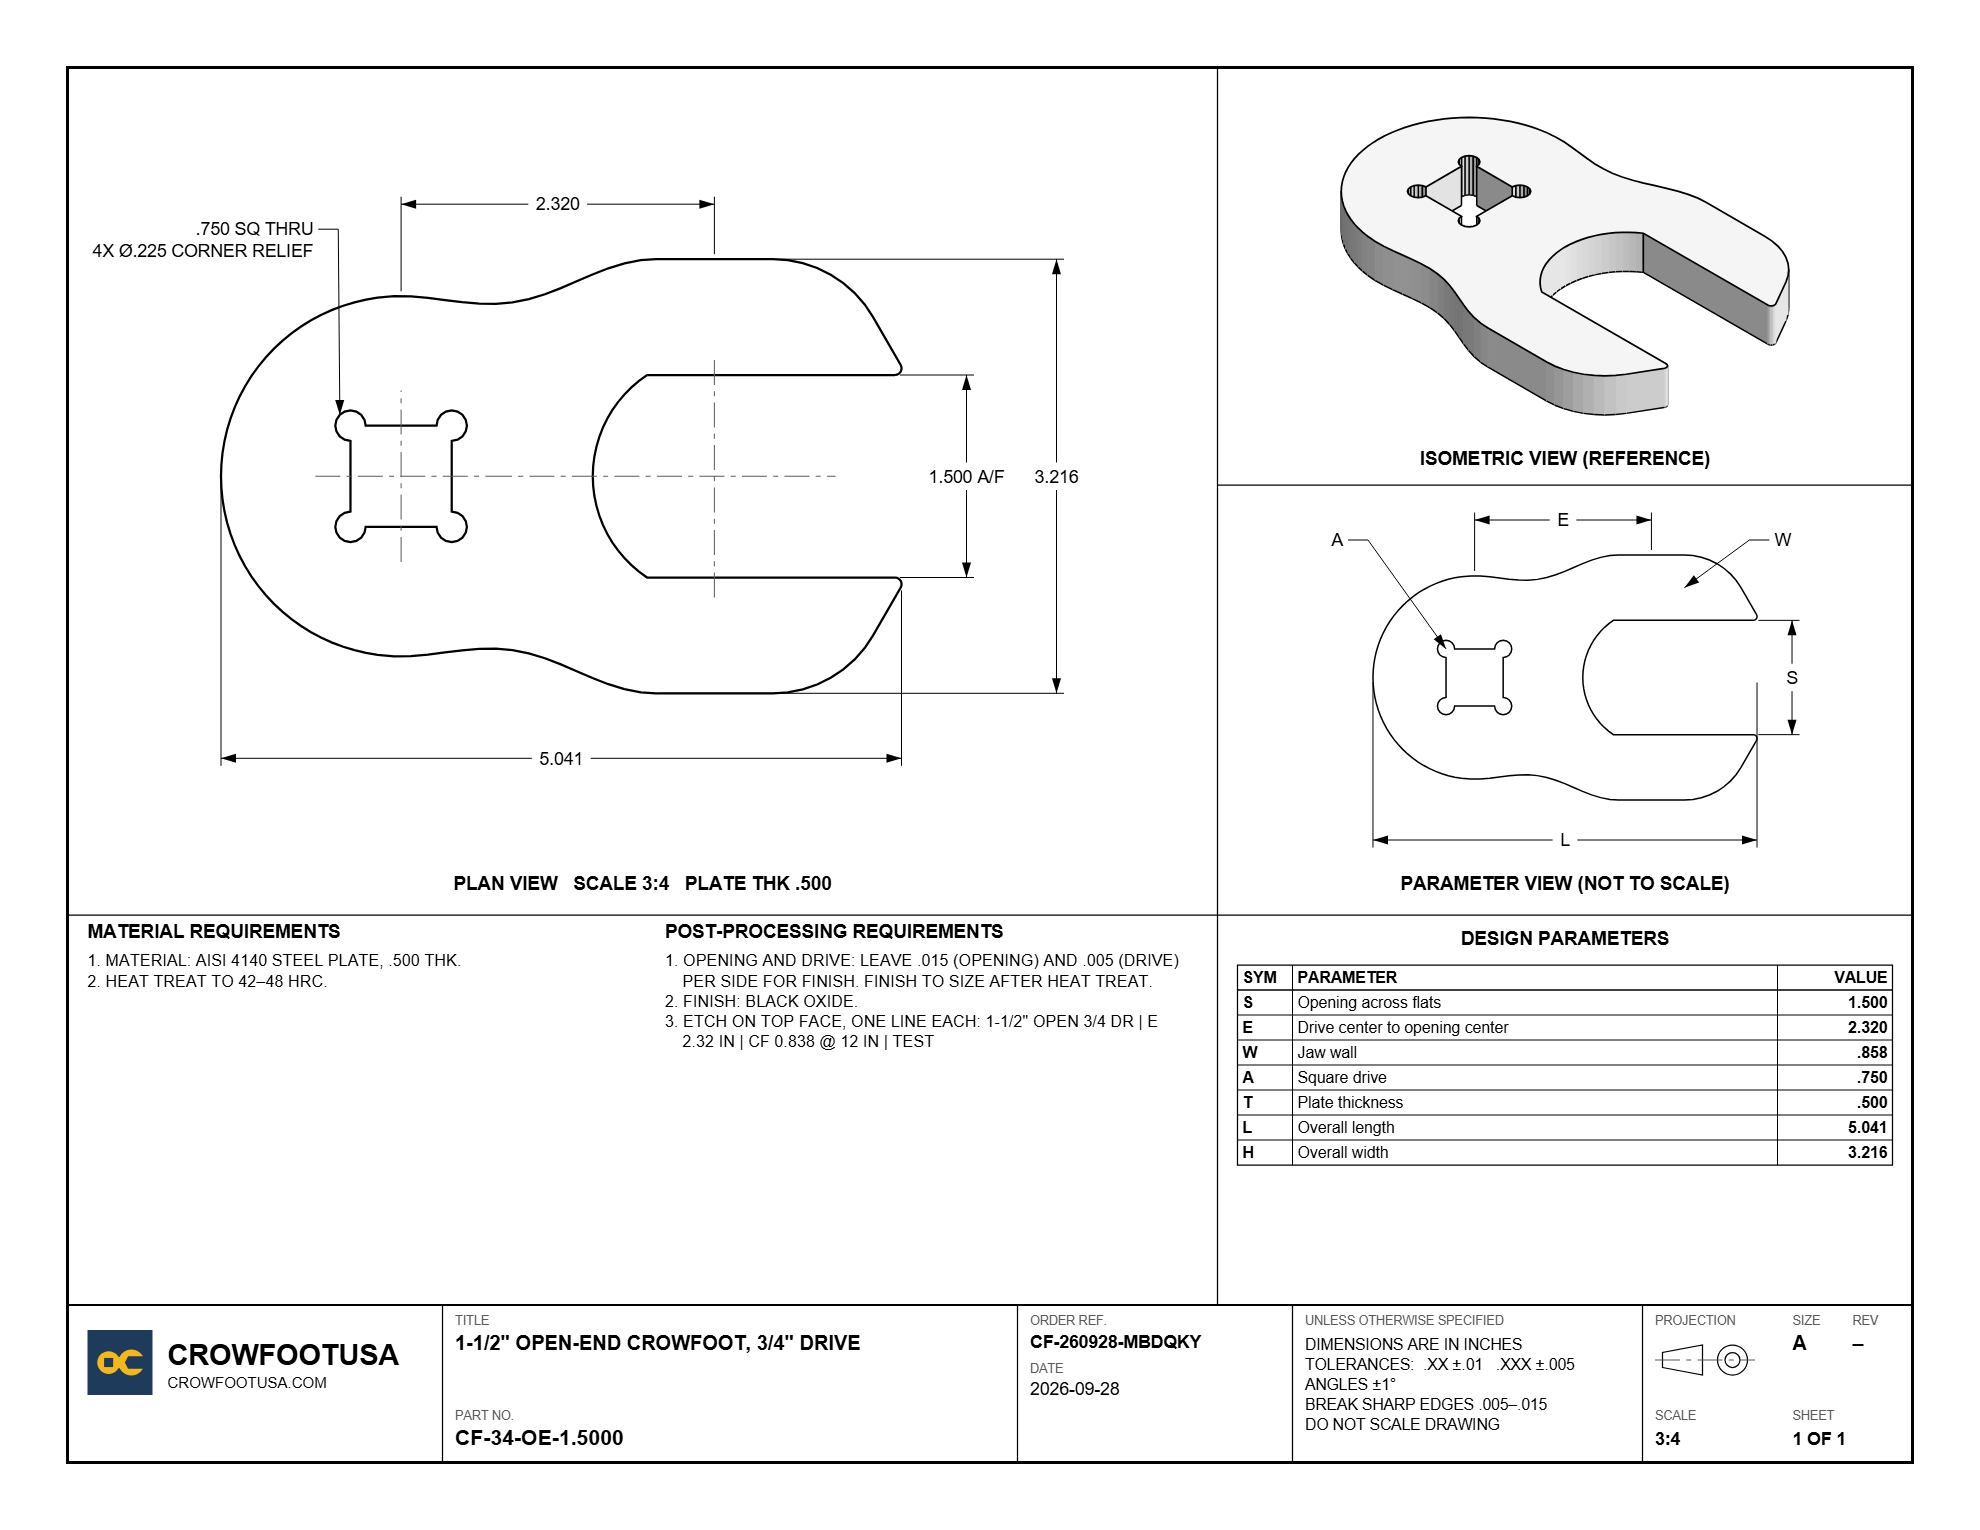
Engineering drawing of part CF-34-OE-1.5000, a 1-1/2 inch open-end crowfoot wrench on a 3/4 inch drive, with plan, isometric and parameter views and material and post-processing requirementsOpen full-size drawing ↗
EV Battery Module Assembly

Machine Vision System Rebuild: Cycle-Time Reduction & Yield Recovery

Machine vision ground-up rebuild across EV battery assembly lines. Eliminated 100% of cycle-time starved time (91%) and recovered 1% process yield (9%).

100%

Starved Time Eliminated

$631.4M

Vehicle Sale Value

+1%

Process Yield

Show full case study: situation, task, action, result
SSituation
BeforeAfter
  • Six EV battery module assembly lines running at capacity
  • Sub A/B: adhesive dispense + profilometer inspection via overhead vision gantry
  • One AutoAssembly cycle = one module; any Sub A/B failure loses one unit
  • 6 lines × failure rate = 240 cars/week exposure
TTask

Dual Bottleneck Identified

1.

Cycle-Time

Sub A/B cycle time exceeded the line bottleneck, starving downstream stations

2.

Yield

Components failing inspection reduced available throughput

Gantry Path: Cycle Time Split

Manual Ingress
4%
Conveyance To Dispense
12%
Adhesive Dispense
43%
Profilometer Inspect
32%
Conveyance From Dispense
9%

Adhesive Dispense + Profilometer = 75% of path time. Inspection travel reducible by 2/3.

Required Outcome

Rebuild the system ground-up: eliminate 100% of starved time, recover 1% yield, integrate all 6 line variants without halting production

AAction

Root Cause Analysis: 8 Identified

×Image Validation Issues
×Inspection Programming is Convoluted and Ineffective
×Visualization is Ineffective
×Data Meaningless
×Mechanical Issues With Gantry
×Fixtures Maintenance
×Subcomponent Quality Issues
×Troubleshooting Requires Engineering to Deep Dive each failure

Ground-up rebuild eliminates these failure modes and enables structured categorization for reaction planning, recovering 1% process yield.

System Integration: 14 Interdependencies

→Vision programming
→Simplified movements
→Conveyance control interlocks
→MES API integration
→Mechanical gantry changes
→Useful data collection
→Feedback Control Loops
→Clear failure mode definitions
→Effective visualization
→SPC alert
→Python bot alerts
→Useful reaction plans
→Effective troubleshooting documentation
→Effective training

Fixturing Design & Gantry Improvements

1.Custom fixturing for 6 line variants with differing mechanical configurations
2.Duplicate system built to run parallel to live production line without interrupting output
3.Developed gantry motion, image tuning, triggering sequencing, storage, networking

Inspection Programming

1. Define Failure Modes and Severities

Critical to Quality of Product

Critical to Yield of Station

2. Develop Inspection Techniques

1. Fundamental Program Architecture, PLC Inputs, Vision Tools, Variable Maintenance

2. Data Collection Logic

3. Data Storage Array Logic

4. Data Conditioning Logic

5. Communication and Storage Logic (PLC and Global)

6. Part Disposition Logic

7. Visualization and SPC Logic

15-Step Script Architecture

1Locate Part Location by Edge
2Locate Inner Fiducial Markers
3Calculate Geometries
4Generate Inspection Regions
5Profile Validation
6Profile Measure
7Special Feature Validation
8Special Feature Measure
9Foreign Object Measure
10Inspection and Image Loop
11Array Variable Data Storage
12Data Conditioning
13Data Judgement
14Communication to PLC
15Communication to FTP

System Validation / Process Control / Management Tools

Gauge R&RFault InjectionProcess QualificationControl PIDSPC and Data VisualizationHMIAutomated Python Alerts
RResult

100%

Starved Time Eliminated

240

cars / week

6 lines

+1%

Process Yield

Vehicle Sale Value

$631.4M

12,480 carsets / yr

91%

From cycle time

9%

From yield

Implanted Medical Device Battery

5× Production Rate Planning: OEE Modelling & Automation Strategy

OEE model and automation roadmap to scale implanted medical device battery production 5× — to 1,113 units/day across 10 processes.

1,113

Units / Day

5×

Capacity Increase

10/10

Processes ≥ Target

Show full case study: situation, task, action, result
SSituation
1× → 5×
  • 10-step implanted medical device battery manufacturing process
  • OEE model: Availability × Performance × Quality; rolling throughput = cumulative FPY × downtime losses
  • 5× demand increase with existing process infrastructure
TTask

Scale to 1,096 units/day. Value stream mapping (VSM) revealed two root capacity failures:

1.

Process Capacity

7 of 10 processes below target; Laser Weld Can Lid is the critical constraint

2.

First-Pass Yield

Powder Metering first-pass yield (FPY) at 45%; the loss compounds across every downstream step

AAction

Strategy Evaluation

Short-Term Bottleneck Management

1,096 /day

  • 3 shifts required
  • +11 headcount, 6 CAPEX
  • Process duplication only
  • Does not address root yield causes

Automation: Selected ✓

1,113 /day

  • 2 shifts only
  • Cycle-time reduction to takt
  • Yield + labor optimization
  • Solves root causes

Cathode Takt

28.15s

Battery Takt

21.89s

Automation Plan: Cycle Time & Yield by Process

CPowder MeteringYield 45% → 95% via automated dispense control; eliminate manual rework loop28.15s
CCathode FormingCycle-time reduction to cathode takt via process parameter optimization28.15s
CSealing and ExcisionAutomated sealing control; cycle-time and downtime reduction to cathode takt28.15s
CInspectionAutomated inspection; cycle-time reduction to cathode takt28.15s
BStack AssemblyAutomated stack feed; cycle-time reduction to battery takt21.89s
BInterior Pin WeldWeld process optimization; cycle-time reduction to battery takt21.89s
BLaser Weld Can LidLaser parameter optimization; cycle-time reduction: eliminates 3rd shift requirement21.89s
BElectrolyte FillPrecision fill automation; downtime reduction; cycle-time reduction to battery takt21.89s
BClose and Terminal WeldAutomated weld scheduling; cycle-time reduction to battery takt21.89s
BLaser Completion WeldCycle-time reduction via parameter optimization to battery takt21.89s
RResult

1,113

units / day

5× demand achieved

2

Shifts

1 fewer than plan A

10/10

Processes

≥ 1,096/day

Key Yield Recovery

Powder Metering

45%→95%FPY

Rolling Throughput / Day by Phase

2100150010966000PMCFSEINSAIPWLWCEFCTWLCWCurrentBottleneck mgmtAutomation
Skin-Graft Surgical Implant

Bacterial Endotoxin Compliance Failure: Facility Recovery Under FDA Scrutiny

BET test method developed and validated under FDA scrutiny. Facility restored in 3 days, quarantined inventory released, Cpk improved from 0.32 to 2.7.

3 Days

Facility Recovery

$4.8M

Revenue Preserved

2.7

Final Cpk

Show full case study: situation, task, action, result
SSituation

Product: Tissue to Skin Graft

Tissue

Processing

Graft

What is Bacterial Endotoxin?

A component of the outer bacterial cell membrane. Sterilization kills bacteria but does not destroy residual endotoxin; it must be quantified directly in the finished implant.

Measured via LAL assay: enzymatic reaction induces clotting; scattered light density measures reaction time.

  • Skin-graft surgical implant; $68M manufacturing facility
  • Under FDA scrutiny, prior qualification methodologies were invalidated
  • No finished-goods Bacterial Endotoxin Test method existed for the product
  • Facility shut down 1 month; product withdrawn from distribution
TTask

Crisis Conditions

Facility shut down for 1 month. Product withdrawn from distribution. Outsourcing of the test initiated.

Recovery plan created and implemented with FDA inspectors on-site.

Required Outcomes

→Develop and validate a Bacterial Endotoxin Test method
→Release quarantined inventory
→Restore production capability
→All under FDA scrutiny

Target Timeline

3 Days

to facility back online

Recovery Framework

1

Patient Safety

2

Method Validated

3

Facility Online

4

Compliance/Cost

AAction

1. Patient Safety: Post-Market Surveillance

→Post-market surveillance: Occurrence rate in complaint history
→% spike recovery: spike sample with known Endo concentration
→95% confidence limit implies 80% 'interference factor' is possible
→Applied correction factor to historic population

2. Test Method Validation

→Strategy to limit scope to 'Worst-Case' by Product Family
→Factors: Age of Animal, Processing Method, Volume, Surface Area
→Reduced unknown interference: Increase dilution
→Rewrote test method
→Corrected direct to FDA observations

Capability Progression

Initial

Cpk 0.32

Ppk 0.33

Triage

Cpk 0.90

Ppk 0.87

Final

Cpk 2.7

Ppk 2.34

BE Validation Criteria

Accuracy

Sample in Duplicate

Linearity

CV%<10%, CC≥0.980

Precision

CV%<10%

Specificity

% Spike Recovery = 50%–200%, PPC CV%<10%

Detection Limit

<0.005 EU/mL

3. Facility Back Online

Quarantine and sustaining lots cleared for release. Second shift added to clear production backlog.

3 Days

Facility Back Online

4. Compliance / Cost Reduction

BET Validation Decision Flowchart

BET TestDilutionTimeVolumeTempAnalyst PerformancePipetting · Reagent PrepAccuracyLinearityPrecisionSpecificityDetectionLimit?NO?NO?NO?NO?NOYYYYYValidated Process

Monitoring Reworks Per Day

0358InitialTriageFinal

Spike Concentration Recovered

USL0.5LSL0.2501.0InitialTriageFinal

Saved 2 hours of test time per day. Second shift QC implemented, doubling throughput. Facility prepared for FDA audit.

RResult

3

Days to Facility Online

$1.2M

Released

$3.6M

Saved

Revenue Preserved

$4.8M

Final Capability

Cpk0.32→2.7
Ppk0.33→2.34

Rework Reduction

Per day4–7→≈ 0
Implantable Battery Backfill Process

Battery Electrolyte Backfill Optimization: DMAIC Yield & Downtime Recovery

DMAIC project recovering yield from 95.4% to 99.6% on implantable battery electrolyte backfill — root causes eliminated across pneumatic, vacuum, spool valve, and operator variation.

99.6%

Process Yield

$770K

Annual Cost Savings

+4.2%

vs 3.6% goal

Show full case study: situation, task, action, result
SSituation
DefineMeasureAnalyzeImproveControl

Problem Statement

Yield95.4%
Scrap cost$1.045M/yr
Downtime24 hr/mo
Downtime cost$741K/yr
  • Implantable battery electrolyte backfill; 0.020 mg process window
  • Weight Low NC = 89.6% of all nonconformances
  • Goal: +3.6% yield, reduce downtime to 3hr planned PM, save $692K scrap + $648K throughput
  • Timeline: DMAIC executed to April 2025
TTask

Process Map: Backfill Sequence

FixtureVacuum1ElecFill 1Vacuum2ElecFill 2Ctrl: Elec Pressure · Spool Valve · Vac Pressure · Elec Batch

Nonconformance Pareto

1007550250Wt Low89.6%Equip Dn5.4%Wt High2.5%Other2.5%n=713
AAction

Measure: MSA & Process Capability

Gauge R&R

Part-to-part exceeds within-operator → measurement system adequate

Special cause: Operator 3 introducing variability

I-MR Control Chart

Special causes identified · Clear process shift · Bimodal distribution

Window: 0.020 mg

Analyze: Root Causes (Multi-Vari & DoE)

×Batch variation: leaking electrolyte tank (removed)
×Vacuum pressure variation: leaks identified and fixed
×Spool valve misalignment: corrected
×Nozzle alignment inconsistency: pneumatic cylinder redesigned
×Airflow variability on spool valve: standardized with fixed orifice
×Operator 3 special cause: addressed via training & cable mgmt overhaul

DoE Top Factors (Pareto of Effects)

B
Spool Elec→Vac
A
Electrolyte Pressure

Improve

↑Redesigned pneumatic cylinder for nozzle alignment
↑Fixed orifice on spool valve: standardized airflow
↑Standardized vacuum & electrolyte pressure setpoints
↑Cable management overhaul: eliminated interference

Control

→Troubleshooting guide + reaction plan
→Standardized PM kits
→Trailing 50 measurements returned to PLC for auto-SPC
→Cathode forming improved to reduce incoming mass variation
RResult
95.4%→99.6%

Process Yield

+4.2%

vs 3.6% goal

$770K

Cost savings

Final Capability

Cpk (within)1.01
Pp0.97
Ppk0.90

Failure Rate

4.6%→0.4%

Downtime

Per month24 hr→3 hr PM